


Reliable Chinese & Vietnam Drive In Rack Manufacturer
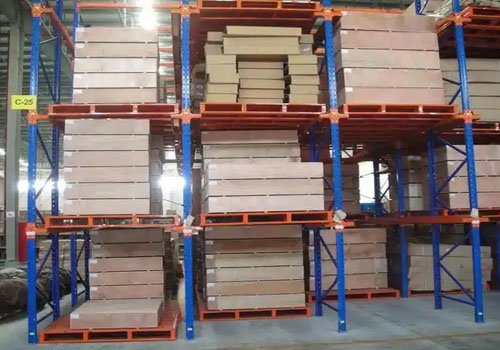
Drive in Pallet racking system is one storage system which have high storage density. The structure of derive in racking is different from other racking system. The post structure mainly take side and vertical loading. All pallets are put on the support arm rail directly which connect with post. It’s the best and most common way to store pallets when you have a lot of the same product
T Racking’s drive-in racking system provides the space efficiency and high volume storage of block stacking, with easy access to pallets. There are no aisles and no cross beams, providing maximum space efficiency. And because each pallet sits on its own support rails, pallets are no longer stacked on top of each other.
Witt the help of multiply manufacturing base in China and Vietnam ( For USA and Australia which have anti dumping tax against pallet rack form China) , T Racking ship drive in racing to customers all over the world effectively.
T Racking offer 10 year’s quality guarantee for of our drive in rack system. Our drive in and drive through rack system comply with SEMA and RMI standard. Extra Free rack inspection is available for of our customers.
Drive In Rack By Feature




Drive In Rack By Application


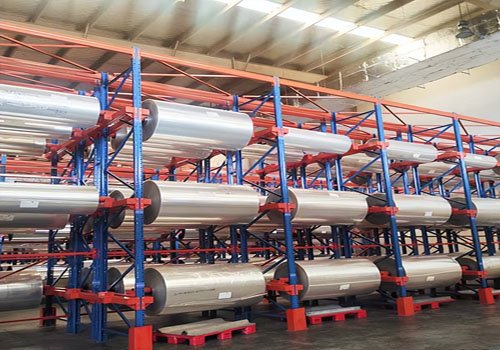


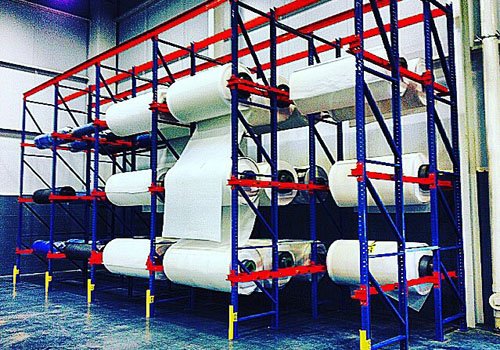
Different types of drive in racking
There are basically two main types of drive-in racking systems:
- Single entry racks: with forklift access to one side only, work for FILO(first in last out)
- Double entry racks(Drive Through Rack): with forklift access from both sides. A large beam is used in the center in order to hold a row of racks in the place. work for LILO(last in last out)


Drive In Racking Structure Detail
Upright Frame: the major support structure for the whole system, consist of upright post, diagonal bracing/horizontal bracing, row spacer…etc
Top Beam: on the top of each bay to hold the comple drive in racking system
Top Bracing: X style bracing on top of each bay, connect by turn buckle or bults & nuts.
Double Support Arm: used in additional bay to hold pallet rail (support arm rail)
Single Support Arm: used in start bay and end bay to hold pallet rail(support arm rail)
Support Arm Rail: the pallet rail which hold the pallets in racking system
Post Protector: to protect forklift from damage the post, this is very important component for drive in racking safety.
Floor Guide Rail: this rail is to guide the forklift driver to move safely in the racking system. It can stop forklift wheels before hit the racking system. This is additional component but we suggest it used in each drive in racking and drive through racking project.
Advantages of Drive In racking
√. Maximize storage capacity by reducing aisles, 85% more storage capacity compare with selective rack.
√. Provides you with an unlimited depth of storage up to 20 pallet deep.
√. Cost Efficiency: reduce warehouse rent cost and energy cost for cold store. cost per pallet about $30-40$ USD
√. Bulk Storage Solution: Great for storing large amounts of the same SKU, suit for seasonal goods storage
√. LIFO Naturally supports Last-In-First-Out inventory rotation
√. Structural Benefits: Less component required, can be custom designed for your forklifts and pallets.
√. Particularly valuable in cold storage/freezer environments
√. It can be used with push back pallet racking in order to build a combination system.


Drawback Of Drive In Racking
- Restricted access to pallets (LIFO system only). You must remove front pallets to get to interior ones.
- Require experience and careful forklift driver: Width of lane is very limited, frequent impacts may weaken the structure.
- Increased time required for loading and retrieving pallets. May lead to stock rotation issues with date-sensitive products.
- Requires specialized forklifts with the right dimensions.
- Hard to implement in warehouses with different pallet sizes.
Suitability Of Drive In Racking
√. Homogeneous SKUs with high pallet number(e.g., beverages, chemicals. food, packing material)
√. Cold/freezer cold chain storage (reduces energy cost in cold store)
√. Urban warehouses with high warehouse rent cost.
×. Not Recommended For: Warehouses with a lot of SKUs or with high selective picking out requirement.

Design and Safety Factor Of Drive In Rack
When you design drive in rack system, please consider below factors:
Depth and Height Limits: Usually 5–10 pallets deep; 4-6 pallet high. The height is usually less than 12 meter, which is the maximum lifting height for most forklifts.
Forklift Compatibility: Requires narrow forklift or stacker to pass through drive way; Usually width of forklift is no more than 1200mm
Critical Safety Features:
√. Floor Guide rails is required to prevent forklift damage
√. Post protector is an extra production for frame
√. Only use quality steel or plastic pallet for drive in racking. As there isn’t beam under the pallet, the loading capacity and strength of pallet used for drive in rack is higher compare with other racking system.
√.Regular inspections and replace damaged parts
√.Carefully operation: driver must drive carefully & slowly especial when enter the rack system.
×. Careless driver may lead to racking impact or potential collapse.
If you have enough budget, consider the ROI rate, pallet shuttle racking is a good alternative solution compare with drive in racking
 EN
 ES
 FR
 PT
 DE
 IT
 RU
 JA